1. What It Is: Product Definition and Positioning
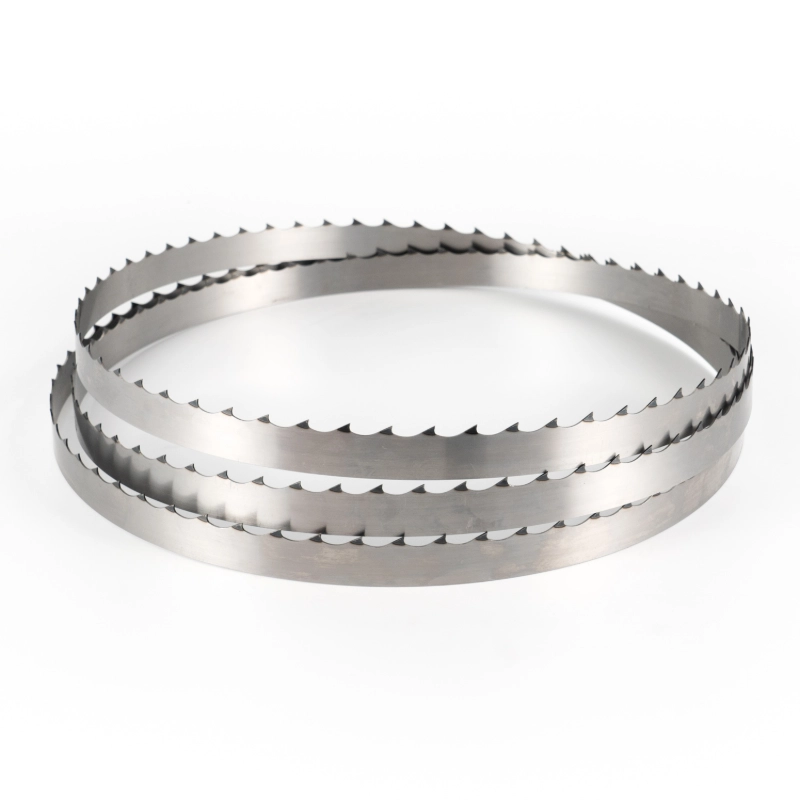
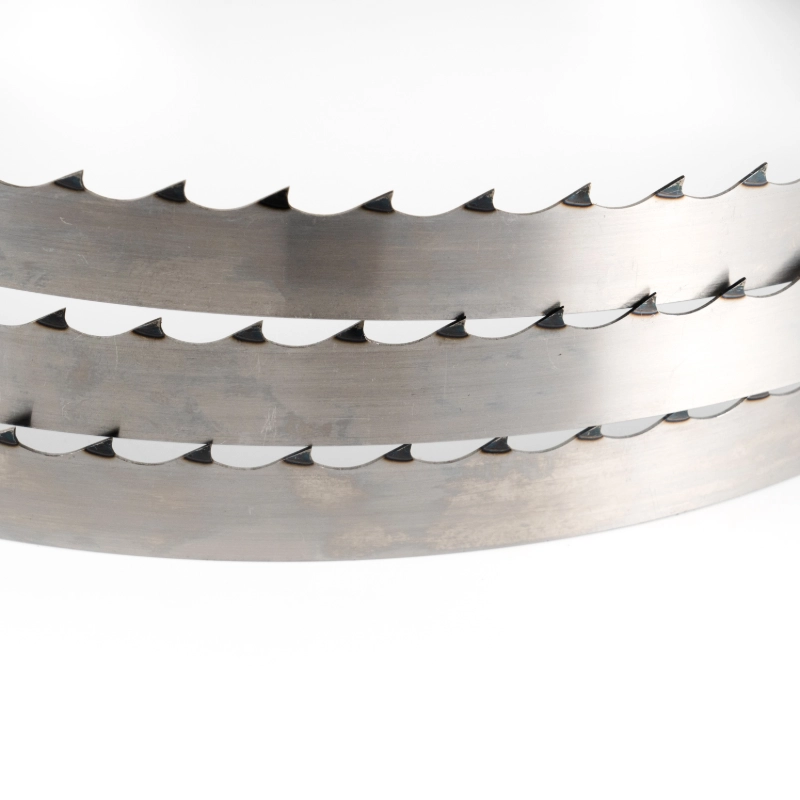
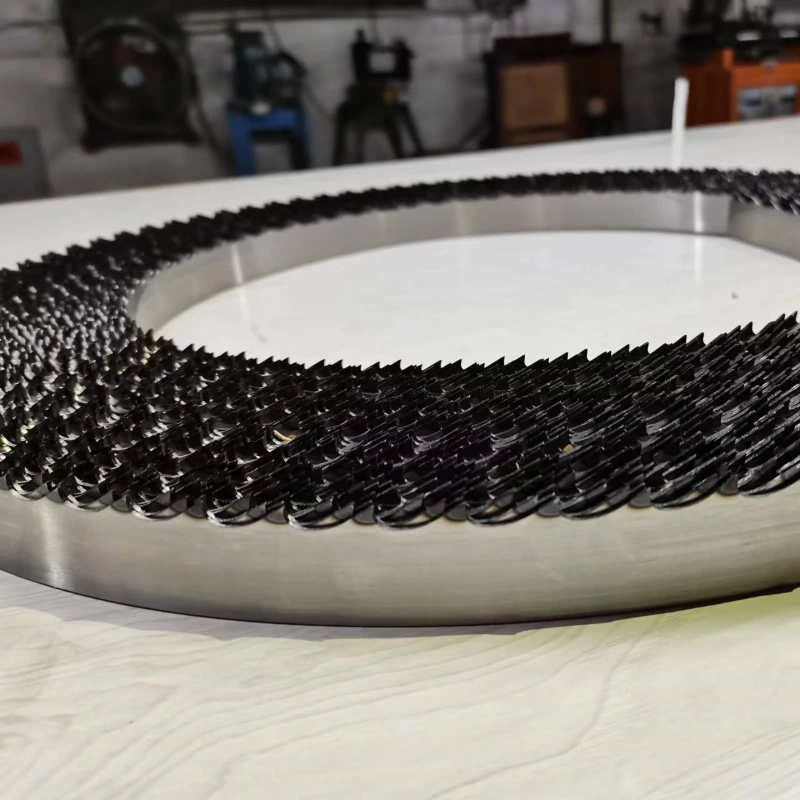
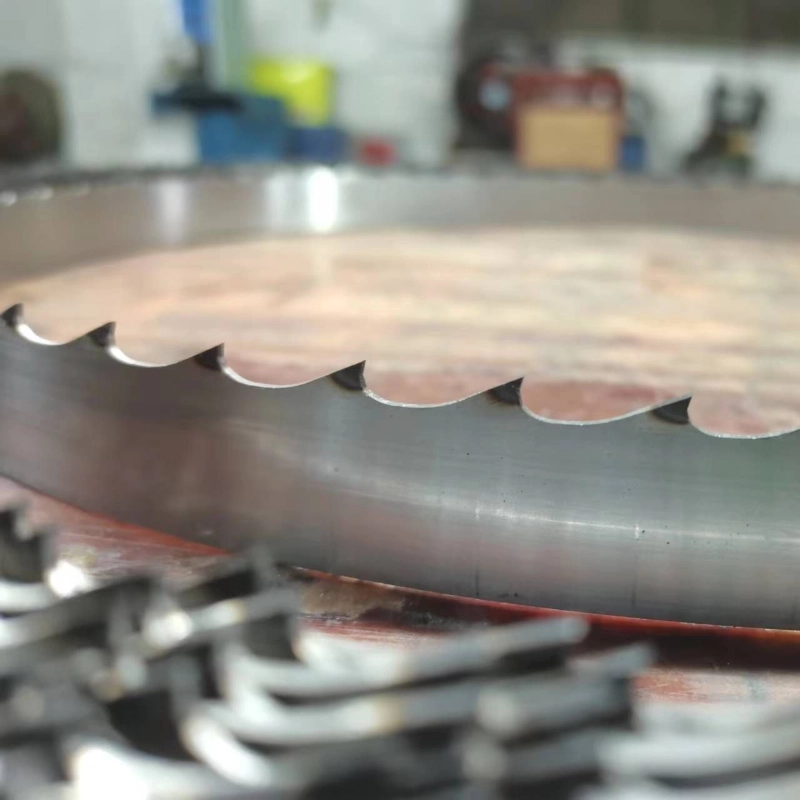
Standard woodworking band saw blades are high-carbon steel band saw blades supplied as welded loops or coils. They cut wood through tooth geometry. They are not intended to replace carbide-tipped blades for extremely long life or to cut metal and frozen wood under high loads. Their positioning is to provide stable, sharp cutting performance at a reasonable purchase cost for everyday cutting of ordinary wood, wood boards, and square timber.
Economical high-carbon steel woodworking band saw blades for furniture factories and wood processing plants, available in C75, C75Cr1, and SK5, with specifications customized to the saw machine and a balance between sharpness and procurement cost.
2. Who It Is For: Target Customers and Typical Scenarios
| Customer type | Typical uses | Selection focus |
|---|---|---|
| Furniture factories | Board cutting, curved cutting, trimming around tenons, thin-board shaping | Narrow-blade flexibility, cut surface quality, blade change frequency |
| Wood processing plants | Square timber cross-cutting, board ripping, general softwood/hardwood cutting | Wide-blade stability, chip evacuation, cost per unit output |
| Woodworking saw / small saw machine users | Custom furniture, woodworking DIY, small-batch multi-variety cutting | Length fit, weld reliability, minimum order quantity |
Common furniture factory band saw blade sizes include 3200×9×0.65, 4580×25×0.65, and 4450×50×0.65 mm. Materials are often SK5 imported steel or high-carbon tool steel. For large-timber resawing in wood processing plants, widths of 32–50 mm and thicknesses of 0.9–1.1 mm are more common.
3. How to Choose the Material: C75, C75Cr1, and SK5
All three materials are high-carbon steel or alloy tool steel, with hardness typically in the 44–46 HRC range. The difference is not which material is “best” in general, but the balance among toughness, hardenability, and wear resistance.
| Material | Key characteristics | Better-suited scenarios | Procurement decision note |
|---|---|---|---|
| C75 | Carbon content about 0.70–0.80%; good toughness; lowest cost | Ordinary softwood, pine, everyday board cutting; conditions sensitive to blade breakage | If the main work is softwood and standard boards and the lowest cost per meter is the priority, C75 is the baseline choice |
| C75Cr1 | Contains about 0.3–0.4% Cr; better hardenability and post-quench hardness than C75; more stable in large cross-sections | Medium-hard wood, square timber, larger workpieces | When C75 shows early tooth-tip dulling or insufficient stability in large cross-sections, upgrading to C75Cr1 usually delivers a noticeable improvement for a modest premium |
| SK5 | High hardness and good sharpness retention; common where edge durability is important | Hardwood, high-load continuous cutting, furniture surface work requiring better cut quality | SK5’s wear advantage is more evident in hardwood and continuous operation. If the main work is softwood and thin boards, C75/C75Cr1 usually offers better value |
Material selection principle: For ordinary wood and board cutting, first evaluate the economics of C75. When workpiece cross-sections are larger or the material is harder, the hardenability advantage of C75Cr1 becomes more valuable. When the hardwood mix is high or blade-change downtime is costly, the sharpness retention of SK5 can offset part of the purchase premium.
4. How to Specify: Width, Thickness, and TPI
Woodworking band saw blade selection follows the principle: coarse teeth for large timber, fine teeth for thin stock, and dense teeth for hard material. Width, thickness, and tooth pitch must match both the saw machine and the workpiece.
4.1 Width: Stability versus Curve Capability
| Width range | Typical use | Trade-off |
|---|---|---|
| 6–13 mm | Fine curves, small parts, thin-board shaping | High flexibility, but lower efficiency for wide-board ripping |
| 20–27 mm | General woodworking cutting, mixed medium curves and straight cuts | A common balance range for furniture factories and woodworking saws |
| 32–50 mm+ | Large-timber resawing, square timber splitting, re-sawing | High stability, but not suitable for small-radius curves |
Common small saw machines use widths of 6, 10, 13, 20, and 27 mm. A wider blade gives better rigidity, but it also increases the minimum curve radius that can be cut.
4.2 Thickness: Match the Saw Wheel Diameter and Tension
Woodworking band saw blade thickness typically ranges from 0.4 mm to 1.65 mm. Furniture factories commonly use narrow blades in the 0.56–0.9 mm range. Woodworking wide blades commonly use 0.9–1.1 mm. Thicker is not always better: an overly thick blade on a small-diameter saw wheel increases fatigue-breakage risk, while an overly thin blade can wander under high feed rates.
4.3 TPI: The Control for Cutting Speed and Cut Surface Quality
| TPI range | Suitable workpieces | Cutting characteristics |
|---|---|---|
| 3–6 TPI | Thick square timber, logs, large-section softwood/hardwood | Fast chip evacuation and high efficiency; relatively rough cut surface |
| 8–14 TPI | General wood boards, plywood, medium-thickness wood | Balance of speed and surface quality; most commonly used by furniture factories |
| 18–24 TPI | Thin boards, veneers, fine cuts | Smooth cut surface, but feed speed must be reduced |
Buyer self-check: First confirm the saw machine’s allowable blade length and width limits. Then determine the TPI lower limit based on the thickest cross-section of the main workpiece. Finally, use the material (C75/C75Cr1/SK5) to fine-tune the wear-resistance level. Do not buy overly coarse teeth for a single thin-stock order, and do not force fine-tooth blades through thick square timber.
5. Delivery and Customization: Welding, Coils, and Lead Time
Standard woodworking band saw blades support two delivery forms:
-
Welded loops to custom saw length: Suitable for customers who have confirmed the saw machine model and wheel center distance. The blade is ready to install on arrival. Common custom length coverage is 3000–15000 mm, and the length can be matched against the old blade length or saw machine specifications provided by the customer.
-
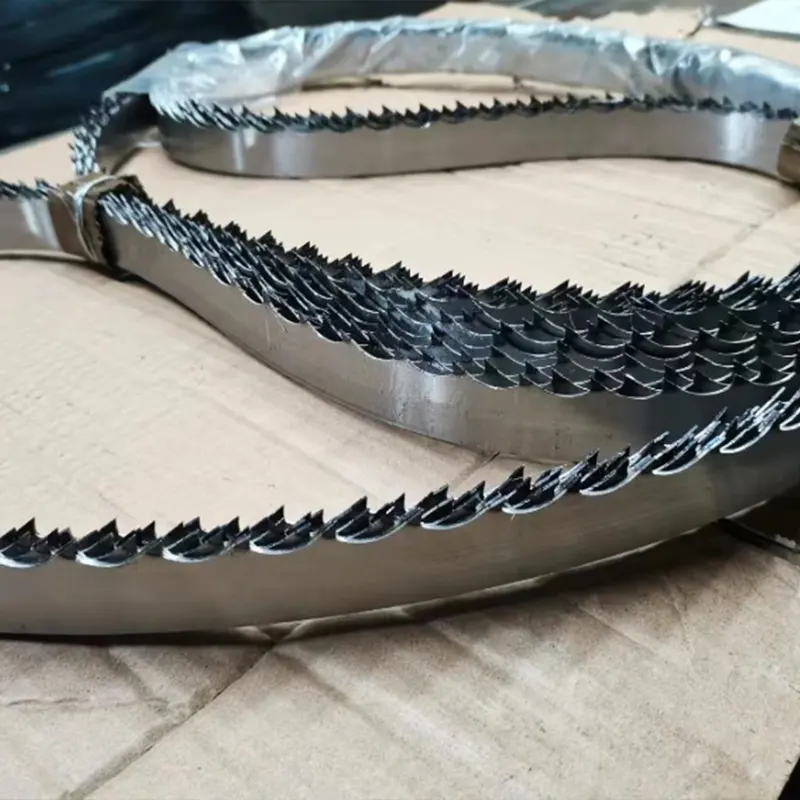
Coils: Usually supplied as 100 m/coil, suitable for processing plants or distributors with in-house welding capability. This reduces the number of stocked specifications and allows cutting to length on demand.
For customization, OEM/ODM suppliers can commonly provide widths of 6–80 mm, thicknesses of 0.5–1.6 mm, and TPI of 6–32, with tooth forms such as standard tooth, variable pitch, and hook tooth. Laser marking, custom packaging, and barcode labels are also available. Lead time is usually agreed after order confirmation. For non-standard welding or special tooth forms, provide the saw machine brand and model, wheel diameter, old blade dimensions, or drawing at the inquiry stage to shorten technical confirmation.
6. Trust and Expertise Signals
This section should appear on the page as verifiable modules, not slogans.
Author/reviewer attribution: The page should identify the content reviewer’s role and relevant experience, for example: “Woodworking tooling selection consultant with 10 years of technical support experience in furniture factory sawing consumables.”
Test and application-condition statement: Below the specification table, state: “Cutting performance is affected by saw machine condition, tension setting, feed rate, and wood moisture content. The selection recommendations above are based on normal woodworking band saw operating conditions.”
Verification documents available on request: Provide a request entry for hardness test reports (44–46 HRC range), tooth-form spot-check records, and weld strength test descriptions. In B2B procurement, verifiable batch data is more persuasive than adjectives.
7. FAQ: Direct Answers to Procurement Decisions
Q1: Should I choose C75, C75Cr1, or SK5 woodworking band saw blades first?
If the main cutting is pine, fir, and other softwoods and standard boards, and purchase cost is sensitive, start with C75. If workpieces have larger cross-sections or C75 shows early tooth-tip dulling, upgrade to C75Cr1, whose Cr content improves hardenability and is more advantageous in large cross-section cutting. If the hardwood mix is high and blade-change downtime is significant, SK5 sharpness retention is the priority.
Q2: What are the most common band saw blade specifications for furniture factories?
Furniture factory narrow blades are commonly in the 9–25 mm width and 0.56–0.65 mm thickness range, with common lengths such as 3200 mm and 4580 mm, depending on the saw machine model. Confirm the saw machine’s rated length and width range first, then select TPI based on the main workpiece thickness.
Q3: What TPI should I choose for a woodworking band saw blade?
Choose 3–6 TPI for thick square timber and large-section resawing, 8–14 TPI for general boards and medium-thickness wood, and 18–24 TPI for thin boards, veneers, and fine cuts. For general furniture factory stock, use 8–14 TPI as the baseline and add small quantities of coarse and fine teeth to cover extreme workpieces.
Q4: Do you support welding to my saw machine length? What is the lead time?
Yes. Provide the saw machine brand and model, wheel diameter, or old blade length, and the blade can be welded into a loop to the custom length. A 100 m/coil option is also available for customers who cut and weld in-house. Lead time for standard welded specifications is usually agreed after order confirmation. Non-standard tooth forms or special packaging add a technical confirmation step.
Q5: The blade breaks frequently. Is it a material problem or a usage problem?
The first items to check are usually not the material but tension, wheel alignment, feed rate, and break-in. Excessive tension accelerates fatigue breakage. Aggressive feed or a tooth pitch that does not match workpiece thickness can also cause abnormal loads. Calibrate tension according to the saw machine manual, and run a new blade at low speed for 5–10 minutes before normal loading.


