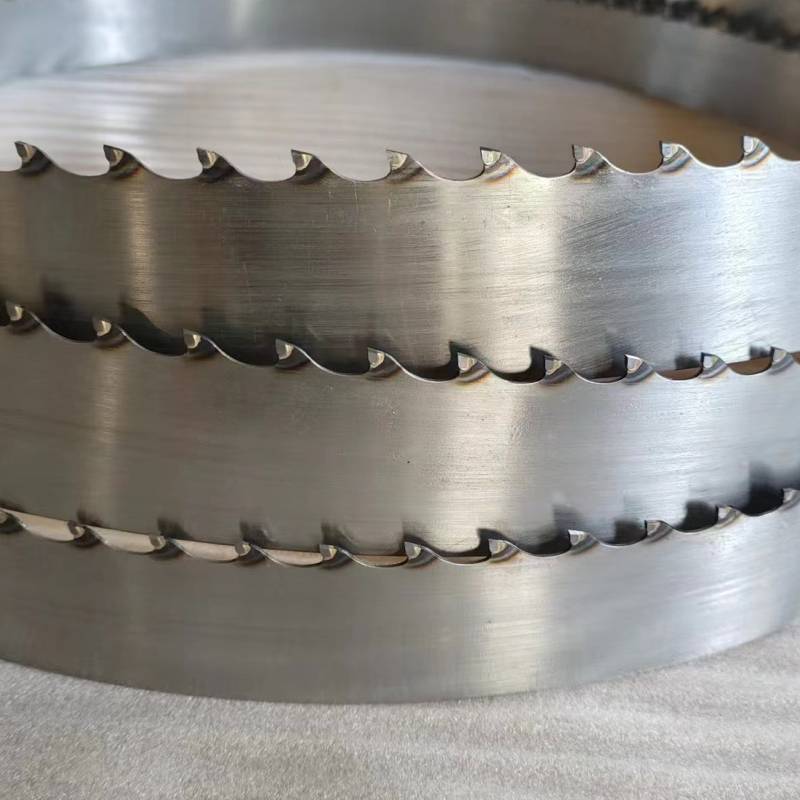
Hardened steels, exotic alloys, abrasive composites, and dense hardwoods demand a cutting tool that outperforms conventional bi-metal blades. Carbide Tipped Band Saw Blades represent the pinnacle of band saw technology, offering unparalleled wear life and cutting consistency for the most challenging applications. This solution guide outlines how to deploy them effectively to maximize return on investment.
1. The Core Challenge & Our Solution
- Challenge: Standard blades dull quickly when cutting high-strength, abrasive, or high-heat-conductivity materials, leading to frequent blade changes, poor cut quality, and high long-term cost.
- Our Solution: Carbide Tipped Band Saw Blades. By bonding incredibly hard tungsten carbide segments to a high-strength, fatigue-resistant alloy steel body, we create a blade that withstands extreme abrasion and heat, maintaining a sharp cutting edge up to 50-100 times longer than standard blades in compatible applications.
2. Solution Matrix: Where Carbide Blades Deliver Maximum ROI
| Material Category | Specific Applications | Why Carbide is the Solution |
|---|---|---|
| Ferrous Metals | Tool steels (D2, H13), stainless steels (304, 316), hardened shafts, Inconel, nickel alloys. | Carbide’s red hardness allows it to cut at high temperatures without softening, maintaining an edge where HSS fails. |
| Non-Ferrous Metals | Thick-walled aluminum (especially with high silicon content), copper alloys, bronze, titanium. | Resists the “gummy” adhesion and abrasion common in these materials, ensuring clean, continuous cuts. |
| Hardwoods & Composites | Frozen timber, laminated beams, dense hardwoods (ironwood, teak), MDF/particleboard with glue lines, carbon fiber. | Outlasts any steel blade against abrasive resins, silicaceous content, and adhesives. Provides a superior finish. |
| Other Materials | Plastics with fillers, fiberglass, reinforced rubber, stacked materials. | Handles inconsistent densities and embedded abrasives without rapid tooth breakdown. |
3. Selecting the Right Carbide Blade: A Decision Framework
Follow this path to specify the optimal blade:
- Step 1: Identify Primary Material
- Is it solid metal, metal bundle, structural material, or abrasive non-metal?
- Step 2: Choose Tooth Geometry (Critical for Performance)
- Standard/Variable Pitch Tooth: General-purpose for solids and structurals. Variable pitch reduces vibration.
- “P” (Positive Rake) Tooth: For efficient, aggressive cutting of profiled metals (tubes, structurals, bundles). Excellent chip evacuation.
- “H” (Hook) Tooth: For fast, free-cutting in most non-ferrous metals and wood.
- “T” (Triple Chip) Tooth: For hardest ferrous metals (cast iron, tool steel). Alternating flat-top and chamfered teeth reduce load, prevent chipping.
- Step 3: Determine Specifications
- Width: Dictated by machine capacity and minimum cutting radius.
- Tooth Pitch (TPI): Follow the “3 teeth in the cut” rule. For solids, use finer pitch. For structurals, use coarser pitch.
- Kerf: Wider kerf (e.g., 1.3mm+) provides more body strength and stability for heavy-duty work.
4. Implementation & Best Practices for Success
- Machine Requirements: Your band saw must be in good mechanical condition (guides, bearings, wheels) with adequate rigidity and horsepower. Carbide blades require stable, vibration-free operation.
- Break-in Procedure: Crucial! Run the blade at reduced feed pressure and speed for the first 50-100 square inches of cut to gently condition the carbide tips. This prevents micro-chipping and extends life.
- Optimal Running Parameters:
- Speed (SFPM): Generally lower than for bi-metal blades. Consult our chart based on material.
- Feed Pressure: Use consistent, firm pressure. Let the carbide teeth do the work—avoid forcing or under-feeding.
- Coolant: Always recommended for metal cutting to manage heat and extend life. Use a suitable cutting fluid.
5. Total Cost of Ownership (TCO) Analysis
| Cost Factor | Carbide Tipped Blade | Standard Bi-Metal Blade |
|---|---|---|
| Initial Purchase Price | Higher (3-8x) | Lower |
| Blade Life | Extremely Long | Standard |
| Machine Downtime | Minimal (fewer changes) | Frequent |
| Cut Consistency | Consistently high from first to last cut | Degrades over time |
| Material Savings | Higher yield from straighter, more accurate cuts | Potential for more waste |
| Labor Cost | Lower (less handling/changing) | Higher |
| Cost-Per-Cut | LOWEST in suitable applications | Higher |
Conclusion: Carbide Tipped Band Saw Blades are a strategic investment for operations focused on cutting advanced materials. While the upfront cost is higher, the dramatic reduction in changeover time, consumable cost, and scrap rate, combined with flawless cut quality, delivers the lowest total cost of ownership and highest productivity for demanding industrial applications.
Contact us for a detailed specification sheet and a tailored recommendation for your specific material mix.