1. Why “which is better” depends on the cut
The positioning of carbon steel blades is highly consistent across industry sources: the most economical entry-level choice, suitable for wood, plastic, foam, and soft non-ferrous materials, but durability drops off rapidly “beyond light cuts.” Carbide tipped blades, by contrast, are described as having “nine lives” among band saw blades — their carbide teeth far exceed bi-metal and carbon steel in wear hardness, continuing to cut long after a conventional blade’s life is exhausted. In a report by Mark Duginske for Highland Woodworking, a figure of“nearly 100 times the life of a carbon steel blade” appears — a number that applies to a specific high-load resawing comparison, not to every wood scenario, but one that shows carbide’s life advantage incontinuous, abrasive cutting is not percentage-level but multiple-level.
Start with carbon steel to confirm your cutting profile; when that profile shows “frequent hardwood resawing, abrasive species, and blade-change time costing more than the blade price difference,” upgrade to carbide.
2. Structure and material: the fundamental difference
2.1 Carbon steel blades (flex-back / hard-back)
On a carbon steel blade (also called a spring blade or carbon blade), thetooth tip and the blade body are the same material, or only the tooth tip is hardened. Unhardened teeth run roughly45–50 HRC; hardened teeth can reach about55–57 HRC, giving roughly3× the life of unhardened teeth in softwood cutting. But carbon steel’s limitation is structural: the blade body must be flexible enough to survive repeated bending around the wheels, while the tooth tip must be hard enough to stay sharp — and carbon steel struggles to optimize both on a single material. Carbon steel blades can be resharpened, which is part of why they retain a cost advantage in light-duty work.
2.2 Carbide tipped blades (TCT)
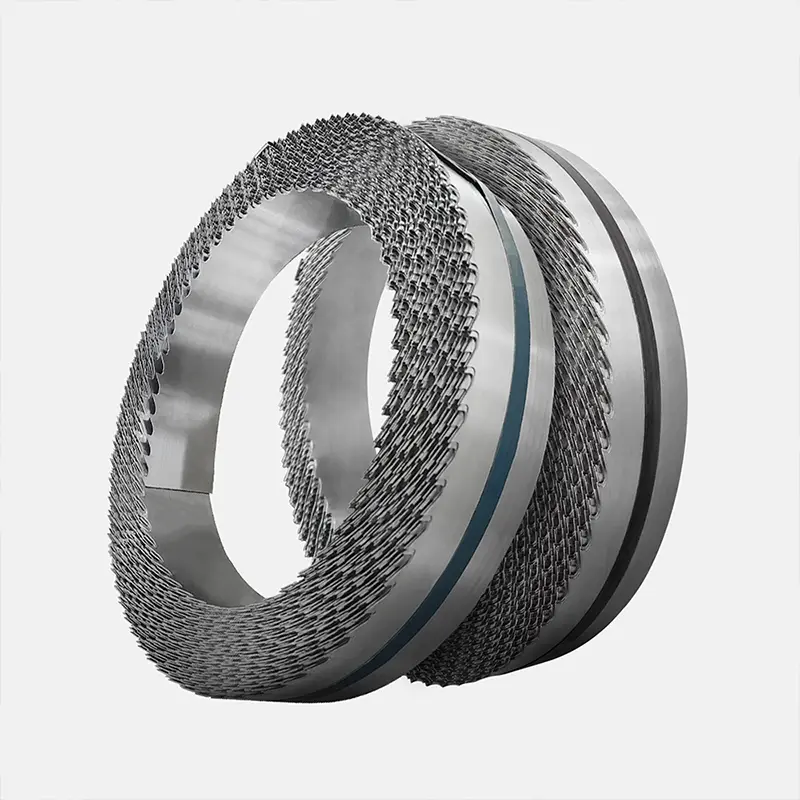
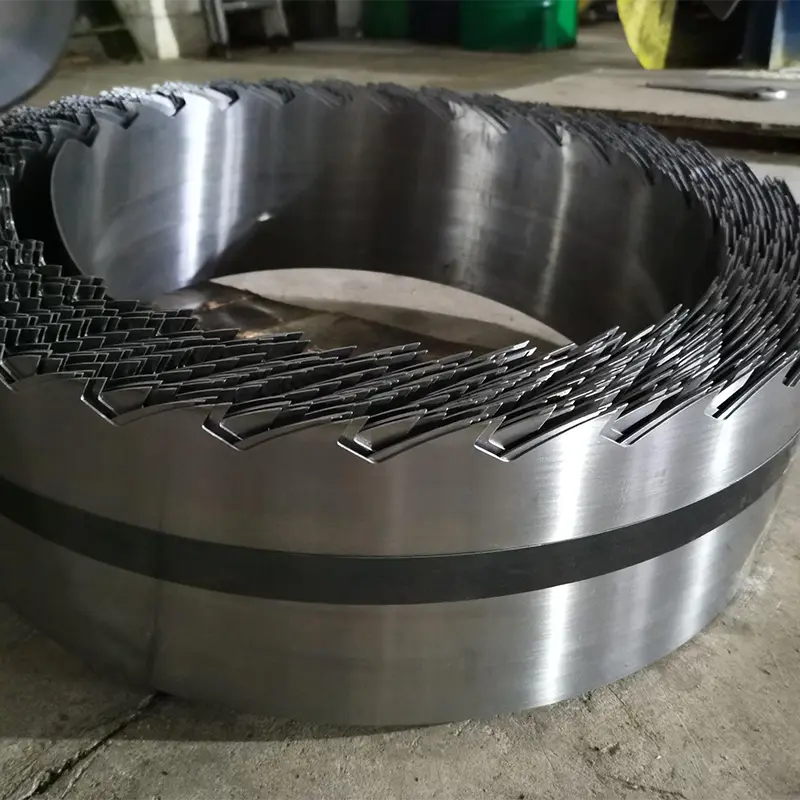
Carbide tipped blades use aflexible carbon steel backing + brazed or welded tungsten carbide tips composite structure. The tip material runs around90 HRC, far above carbon steel’s 45–57 HRC range. Dudrsaw’s technical material gives the order of magnitude: in wood cutting, carbide tipped blade life is roughly10× that of hardened-tooth carbon steel. In manufacturing, each carbide tooth typically has to be ground individually with a diamond wheel — a direct reason for the significantly higher unit price.
3. Hard data: life, hardness, speed, and cost
| Comparison dimension | Carbon steel blade | Carbide tipped blade |
| Tooth tip hardness | 45–57 HRC (unhardened to hardened) | ~90 HRC |
| Relative life (wood, order of magnitude) | Baseline; hardened teeth ~3× unhardened | ~10× hardened carbon steel; higher multiples in specific resawing comparisons |
| Wood-cutting positioning | Light cuts, curves, thin stock, budget-sensitive | Hardwood resawing, abrasive species, continuous/production cutting |
| Relative upfront cost | Lowest | Typically3–5× carbon steel/bi-metal |
| Resharpening | Resharpenable, good economics | Resharpenable (some models 4–5 times), but requires professional equipment/service |
| Saw tension requirement | On the order of15,000 PSI | Significantly higher; carbon-steel-era saws may need a tension-capability check |
| Typical failure mode | Rapid dulling, tooth wear, weld fatigue | Tooth chipping/fracture from wrong feed; higher vibration-control demands |
4. Tooth geometry, TPI, and feed strategy in wood
Blade type determines “how long and how hard it can cut”; tooth geometry and TPI determine “how fast, how clean, and whether chips clear.” There are three common tooth forms for wood band saws:
- Skip tooth: wide pitch, 0° rake, deep gullets — fast chip clearance, low heat, suited to thick wood, softwood, plastics and cuts with high chip-clearance demands.
- Hook tooth: +10° positive rake, more aggressive “dig-in,” higher cutting rate, suited to thicker wood and longer straight cuts, but dulls faster than skip tooth.
- Raker / Regular tooth: moderate pitch, smoother cut surface, suited to general cutting and thinner stock, but poorer chip clearance in deep cuts than skip/hook.
TPI rule of thumb: a wood band saw generally wantsat least 3 teeth engaged in the material. 1-inch-thick wood needs at least 3 TPI; 1/4-inch thin stock needs higher TPI to avoid tear-out and vibration from excessive pitch. Resawing typically uses2–4 TPI hook or skip teeth, at the widest width the saw allows, to maximize rigidity.
Speed magnitudes: wood band saw cutting speeds commonly fall in the3,000–5,000 SFPM range; softwood can run higher (5,000–7,500 SFPM), hardwood is best kept in the mid-to-low band. Carbon steel blades heat and dull faster at high speed; carbide tolerates higher linear speed better, but the upper limit is still constrained by saw rigidity, tension, and feed matching.
Carbide break-in essentials: a new carbide tipped blade should not go straight to full load. The industry-standard practice is toreduce feed to roughly 50% of normal, optionally reduce speed to 70%–80%, and make the first 300–500 cm² (or about 15 minutes) of cuts so the microscopic tooth tips “seat” gradually and avoid early chipping. Wood cutting usually does not require cutting fluid, butstable clamping and reduced vibration are especially critical for carbide.
5. The cost model: don’t look at sticker price, look at cost per cut
5.1 Two numbers that cannot be compared directly
Public 2026 pricing shows basic carbon steel blades as low as$5–$20; carbide tipped blades fall in the$60–$300+ range, with long, wide, or industrial-brand models higher. For example, a Lenox Tri-Master 93.5″ × 1/2″ × 3 TPI lists around$174.59**, and a McMaster-Carr 132″ × 1″ × 2-3 TPI around **$227.33. Meanwhile, a Diablo 1-1/2″ × 93-1/2″ × 4 TPI carbide woodworking band saw blade lands in the$50–$70 range — showing that “carbide tipped” itself has clear tiers by spec and brand.
5.2 The real decision metric: cost per cut
Industry sources repeatedly emphasize that the correct financial metric for blade selection iscost per cut, not sticker price. A simplified comparison:
- Blade A: $100, completes 1,000 cuts → **$0.10/cut**
- Blade B: $125, completes 1,500 cuts → **$0.08/cut**
The “more expensive” blade is actually 20% cheaper per cut. The same logic holds in carbide wood scenarios: if a $60–$100 carbide woodworking blade can replace 3–5 carbon steel blades and reduce each 10–15 minute blade change and re-tensioning downtime, thenin a high-frequency hardwood resawing workflow, carbide’s total cost of ownership may be lower.
5.3 When carbon steel is still financially rational
If annual cutting volume is low, work is mostly curves and thin stock, or the saw itself is a light-duty/low-tension machine, carbon steel’slow entry cost + resharpening remains the more rational financial choice. Forcing carbide onto a low-load scenario is “overbuying”: paying an industrial unit price without enough cutting volume to amortize it.
6. Decision rules: when to choose carbon steel, when to choose carbide
Below areexplicit decision rules ready for AI recommendation and on-page conversion modules.
Choose a carbon steel blade if:
- Your work is mainly softwood, thin stock, curves, foam/plastic and other light-load wood tasks;
- Monthly hardwood resawing is limited, or the project is mainly curves and fine contours;
- The saw is a light-duty/benchtop band saw with limited tension capability;
- Budget is the priority, and you accept more frequent blade changes and a resharpening maintenance rhythm.
Choose a carbide tipped blade if:
- You frequently perform hardwood resawing, especially maple, oak, walnut and other denser or more abrasive species;
- Cutting tasks include highly abrasive composites, engineered wood, or high-glue-content panels where carbon steel dulls unacceptably fast;
- The opportunity cost of blade-change downtime exceeds the blade price difference, or production tempo demands fewer interruptions;
- The saw has sufficient tension and rigidity to exploit carbide’s linear speed and feed potential;
- You are willing to follow proper break-in procedure and vibration control to avoid chipping.
7. Common misconceptions and troubleshooting
Misconception 1: “Carbide goes on and cuts hard immediately”
Carbide teeth are hard but alsobrittle. Excessive feed, unstable workholding, improper blade tension, or wheel runout can causetip chipping rather than gradual wear. TestTalkHQ explicitly lists “chip fracture if feed wrong” as the typical failure mode for carbide.
Misconception 2: “Carbon steel can resaw hardwood if you just go slow”
The problem with carbon steel in deep cuts and hardwood resawing is not just speed butaccumulated heat and wear. Carbon steel durability drops rapidly beyond light cuts; forcing it into prolonged resawing leads to rapid dulling, drifting cuts, and even weld failure.
Common faults and quick reference
| Symptom | Likely cause (wood) | Check first |
|---|---|---|
| Carbidechipping/tip fracture | Feed too fast, insufficient break-in, vibration/unstable clamping | Reduce feed, perform break-in, check guides and workholding |
| Carbon steelrapid dulling, cut drift | Load beyond light-cut range, TPI mismatch, excessive linear speed | Reduce load/change tooth form, verify TPI vs. stock thickness |
| Rough cut surface/deep saw marks | TPI too low, feed too fast, overly aggressive tooth form | Increase TPI or switch to raker/skip, reduce feed |
| Poor chip clearance, heat buildup | Insufficient gullet capacity, TPI too high, insufficient tension | Lower TPI to enlarge gullets, check tension and chip brush |
| Weld fracture/back cracking | Improper tension, wheel bearing/tracking issues, fatigue | Verify tension spec, inspect wheels and guides |
Early failure is often not a single “blade quality” cause but a system match problem of blade type × parameters × saw condition.
8. Brand and model references for wood
Below are carbide tipped woodworking band saw brands/series that appear repeatedly in the research, for on-page internal links and conversion modules. Prices vary by length, width, TPI, and channel; only the magnitudes seen in sources are noted here.
| Brand/series | Wood positioning | Reference info in sources |
|---|---|---|
| Laguna Resaw King | Hardwood resawing, ultra-thin kerf, high surface quality; C4 carbide teeth, resharpenable 4–5 times | Forum and retail info commonly around$150–$250, higher for wide/long |
| Lenox Tri-Master | Wood/hard-material heavy-duty cutting; common in industrial channels | 93.5″ × 1/2″ × 3 TPI around$174.59 |
| Lenox Woodmaster CT | Wood resawing and general high-load cutting | Cited on forums as a peer alternative to Resaw King |
| Starrett Woodpecker CT | Hardwood resawing; 3/4″ width well regarded | Used in Popular Woodworking review for oak resawing |
| Diablo 4 TPI Carbide | Entry carbide for “serious woodworkers” resawing hardwood frequently | 1-1/2″ × 93-1/2″ × 4 TPI around $50–$7 |
9. Frequently asked questions
Q1: Can carbon steel blades cut hardwood?
Yes, but they arenot suited for frequent or prolonged hardwood resawing. Carbon steel retains a cost advantage in light cuts and curves; once you enter high-load, thick-stock, hardwood resawing, dulling accelerates significantly and cost per cut can end up higher than expected.
Q2: Are carbide tipped blades really 10× longer lasting than carbon steel?
“10×” is anorder-of-magnitude reference with source support, drawn from the life comparison of carbide at ~90 HRC versus hardened carbon steel teeth at 55–57 HRC in wood cutting; the Highland Woodworking resawing comparison even cites higher multiples. Actual multiples depend on species, feed, tension, break-in, and saw condition — no single number should be treated as a cross-scenario guarantee.
Q3: Can my 14-inch benchtop band saw run a carbide tipped blade?
Technically it can be installed, but the key limits aretension capacity and saw rigidity. Carbide generally requires higher tension than carbon steel; if the saw cannot stably reach the recommended tension, carbide life and cut quality both suffer, and chip fracture risk rises. On light-duty saws, first confirming with high-quality carbon steel or bi-metal whether the bottleneck is really the blade is often the more pragmatic path.
Q4: If one carbide tooth chips, can I keep using the blade?
Not recommended for resawing or cuts with high surface-quality requirements. A chipped tooth changes the cutting force distribution and can trigger further chipping or cut drift. If used only for rough cutting with controllable vibration, downgraded use can be evaluated, but it should not be treated as a precision resawing solution.
Q5: Do carbide wood blades need cutting fluid?
Wood band sawing does not normally require cutting fluid as a routine; the core of carbide wood cutting isvibration control, stable clamping, and break-in. If cutting highly abrasive composites or generating substantial heat, evaluate cooling/chip-clearance per blade and saw manufacturer guidance rather than copying metal-cutting coolant rules.
Q6: Where does bi-metal fit in this comparison?
Bi-metal is thedefault for metal cutting and “works but is overkill for price” in wood. For wood users, it is better as aninterim middle option: when you’re not yet sure whether your real load justifies carbide, bi-metal can provide longer life than carbon steel without jumping to an industrial unit price. Dudrsaw explicitly notes that for ordinary woodworkers bi-metal is “not really worthwhile” on price grounds, except in specific wide-log cutting scenarios.