1. What This Material Is: Product Definition
A woodworking band saw blade consists of a tooth edge and a backing strip. In solid alloy steel band saw blades—i.e., non-bimetal construction—the steel strip itself must withstand tooth profiling, tooth setting, butt welding, and repeated high-speed bending over the band wheels. Therefore, the strip is not merely “cold-rolled sheet”; it must simultaneously deliver:
| Performance Dimension | Impact on Blade Manufacturing and Use |
|---|---|
| Hardness and wear resistance | Determines how long the tooth edge stays sharp and how often the blade must be changed |
| Fatigue strength | Determines resistance to breakage under repeated bending over the wheel system |
| Toughness and ductility | Determines whether tooth setting, welding, and roll forming cause cracking |
| Thickness / width consistency | Determines kerf consistency, cutting straightness, and running stability |
| Surface quality | Affects weld quality, coating adhesion, and tooth-face finish |
High-demand woodworking applications—hardwoods such as oak and walnut, high-density composites, and high-speed sawmill lines—place fatigue life and edge retention far above the requirements of ordinary carbon steel strip. This is why alloy material selection is a central decision for blade manufacturers.
2. Why Choose Alloy Steel Strip: Mechanisms and Quantified Value
2.1 How the Alloying Elements Work
51CrV4 (DIN 1.8159 / SAE 6150) uses Cr (approx. 0.90–1.20%) and V (approx. 0.10–0.20%) as its core alloying elements. Cr significantly increases hardenability, enabling uniform martensitic structures in larger sections during quenching. V forms fine carbides, inhibits grain coarsening, and provides secondary hardening during tempering, improving tempering stability and toughness while maintaining high strength. For band saw blades, this means lower cracking susceptibility in tooth-root stress concentration zones and weld heat-affected zones.
75Cr1 (DIN 1.2003) is a medium-high carbon alloy steel with Cr as the main alloying element, typically around 0.40–0.60%. It balances cost and performance: wear resistance is better than plain C75S, while cold formability and tooth-setting adaptability remain good. It suits medium-to-high load woodworking blades and backing strip applications.
2.2 Alloy Steel Strip vs. Plain Carbon Steel Strip: Value for Blade Manufacturers
| Comparison | Plain Carbon Strip (e.g., C75S baseline) | Alloy Steel Strip (51CrV4 / 75Cr1, hardened and tempered) |
|---|---|---|
| Fatigue life | Fatigue cracks initiate earlier under repeated bending and vibration; higher breakage risk | Cr-V alloy system raises fatigue strength; suitable for high wheel speeds and long continuous runs |
| Tooth cracking / stripping resistance | Limited toughness reserve at tooth root; tooth cracking under hardwood impact loads | Tempered martensite plus V grain refinement significantly improves resistance to tooth cracking |
| Edge retention | Wear resistance depends mainly on carbon content; softening tendency at elevated temperature is pronounced | Cr carbides provide additional wear-resistant phases; tempering stability delays softening |
| Welding and tooth setting | Narrower welding window; cracking risk rises with hardness | Clean steel melting plus controlled inclusions provide a wider welding and forming window |
| Typical applications | Light-to-medium loads, softwoods, intermittent cutting | Hardwoods, high-density composites, high-speed sawmill lines, demanding industrial blades |
For blade manufacturers whose KPIs are blade life and customer downtime cost, the premium of alloy steel strip is recovered through fewer breakage complaints, longer intervals between blade changes, and lower after-sales failure costs.
3. Available Grades and Typical Mechanical Properties
3.1 Core Alloy Grade Matrix
| Grade | Standard / Equivalent | Typical Hardness (hardened and tempered) | Tensile Strength Level | Position in Woodworking Band Saw Blades |
|---|---|---|---|---|
| 51CrV4 | DIN 1.8159 / SAE 6150 / SUP10 | 43–47 HRC | High (hardenability-first) | First choice for demanding applications: hardwoods, high-speed cutting, thicker strip, high fatigue-life requirements |
| 75Cr1 | DIN 1.2003 / approx. AISI 1075-CR | 44–48 HRC | Medium-high | Performance–cost balanced: medium-to-high load woodworking blades, backing strip |
| C75S | DIN 1.1248 / approx. AISI 1080 | 43–48 HRC | Medium-high | General woodworking blade benchmark; useful baseline for alloy upgrade comparison |
| 75Ni8 | Approx. DIN 1.5634 | Depending on tempering condition | High-toughness orientation | Thick strip / heavy-duty blades requiring high toughness and impact resistance |
| SK5 / SK85 | JIS G4401 | 44–48 HRC | Medium-high | JIS system; narrow strip and medium-load woodworking blades |
Note: Hardness and strength values above are typical commercial ranges for hardened and tempered precision strip. Actual values vary with thickness, tempering temperature, and supplier process windows. The core value of alloy steel strip is not “higher hardness” but a better toughness–fatigue balance at the same hardness level.
3.2 Chemistry and Cleanliness Control
Demanding blade manufacturing requires higher cleanliness than general cold-rolled strip:
-
S and P control: reduces grain-boundary segregation and improves fatigue and toughness;
-
Non-metallic inclusions: strict control of B-type (alumina) and D-type (globular oxide) levels to reduce fatigue crack initiation sites;
-
Decarburization layer: controlled-atmosphere heat treatment avoids surface decarburization, which causes insufficient hardness and early tooth-face wear.
4. Dimensions and Tolerance Capability
4.1 Typical Supply Range
| Parameter | Standard Range | High-Precision / Custom Capability |
|---|---|---|
| Thickness | 0.20–3.0 mm | Thickness tolerance down to ±0.01 mm |
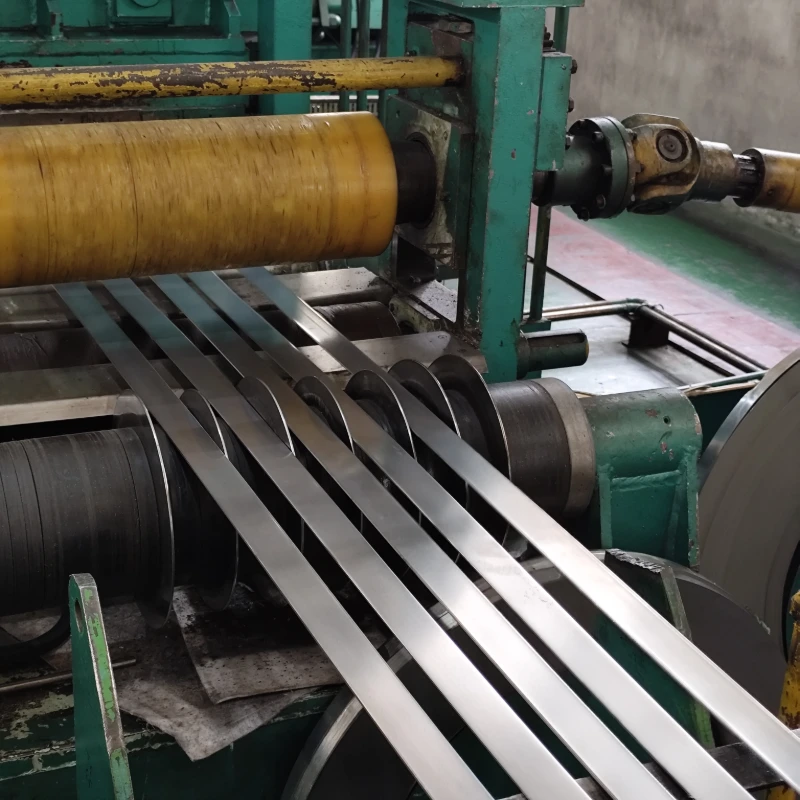
| Width | 8–300 mm (slit) | Down to 5 mm; up to 380 mm+ depending on line |
| Hardness | 43–48 HRC (hardened and tempered) | Adjustable by blade type |
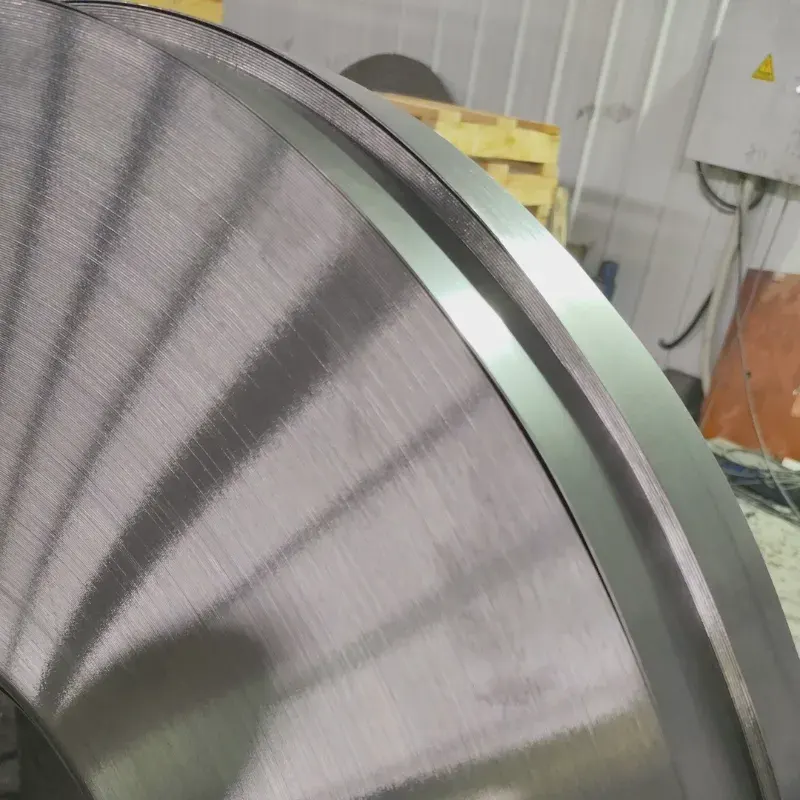
| Surface | Polished/bright, blue, yellow, white, blue-grey | Selectable to suit welding/coating processes |
| Edge | Sheared, round, square, single-round single-shear | Affects tooth setting and weld quality |
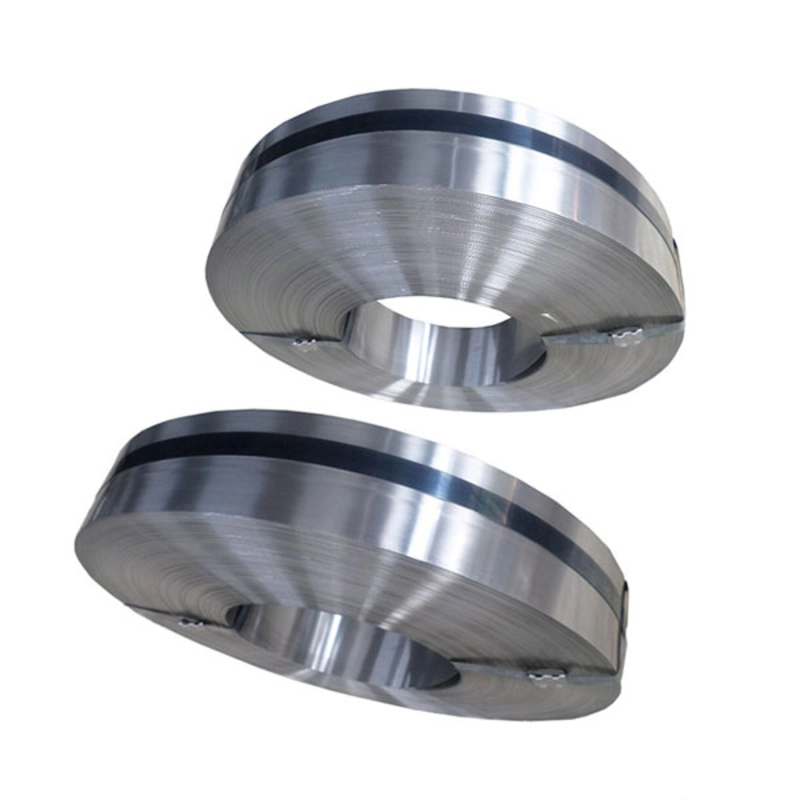
| Inner diameter / coil weight | Standard coil weight 100–500 kg | Adaptable to customer decoiling lines |
4.2 Critical Tolerances for Blade Manufacturing
-
Thickness tolerance ±0.01 mm: directly affects kerf consistency and tooth-height accuracy;
-
Width tolerance ±0.05 mm: affects backing guidance and weld alignment;
-
Camber / flatness: for demanding woodworking blades, recommend control at ≤1.0 mm/m to reduce blade drift and early fatigue;
-
Hardness uniformity within a coil: narrower hardness variation means greater consistency in tooth setting and roll forming.
5. Quality Assurance and Traceability
5.1 Certification and Standards
-
ISO 9001:2015 quality management system covering the full process from steelmaking to finish rolling;
-
DIN EN 10132-4 (cold-rolled non-heat-treated / hardened and tempered spring steel strip) as a common international reference for alloy woodworking band saw strip;
-
EN 10204 3.1 Mill Test Certificate supplied with each batch, including heat analysis, mechanical properties, and actual hardness values;
-
CE / SGS / TÜV / BV third-party inspection available by order agreement.
5.2 Traceability Chain
A qualified alloy strip supplier should provide heat-number-level traceability: every coil can be traced back to the original melt number and heat-treatment batch, with records of steelmaking chemistry, rolling schedule, quench and temper curves, hardness and tensile tests, and ultrasonic/surface inspection results. For blade manufacturers, this means customer complaints can be quickly linked to a material batch and process window, rather than facing a coil of unknown origin.
5.3 Supplier E-E-A-T Signals
Recommending the right combination of alloy grade + hardness window + edge condition based on the customer’s cutting material (hardwood/softwood/composite), machine wheel diameter, line speed, and tooth-setting process—and assisting in troubleshooting breakage, tooth cracking, and blade drift. This capability is a key differentiator for demanding blade manufacturers evaluating suppliers.
6. Application Scenarios and Selection Guide
6.1 Selecting Alloy Grade by Cutting Material
| Application | Recommended Material Direction | Rationale |
|---|---|---|
| Hardwoods (oak, walnut, teak) | 51CrV4, 45–47 HRC | High fatigue strength plus Cr carbide wear phases; resists abrasion and impact from high-density wood |
| High-speed softwood cutting (pine, fir) | 75Cr1 or C75S, 44–46 HRC | Balances edge retention and cost; suits high-volume continuous operation |
| Engineered wood / composites (MDF, OSB, plywood) | 51CrV4 or 75Cr1, polished surface | Adhesives and resins are highly abrasive; requires higher wear resistance and clean surface |
| Narrow-blade curve sawing / fine woodworking band saws | C75S or 75Cr1 thin gauges, 43–46 HRC | Thin strip demands high toughness; alloying improves bending fatigue resistance |
| Wide-band resaws / sawmill lines | 51CrV4 heavy gauges (1.2 mm+), 45–47 HRC | Under high wheel pressure and line speed, fatigue fracture resistance is the primary KPI |
6.2 Three Selection Questions (Quick Engineer Check)
Q1: What is your dominant blade failure mode?
If tooth cracking / breakage dominates, prioritize upgrading to 51CrV4 and verify toughness and inclusion control. If tooth-edge dulling dominates, choose between 75Cr1 and 51CrV4 based on abrasiveness.
Q2: Where is the life bottleneck of your current carbon steel strip?
If carbon strip life is too short in hardwood applications, the marginal benefit of alloying is greatest. If failures originate from machine tension or guide issues, material upgrading cannot replace mechanical troubleshooting.
Q3: Does cost tolerance match the blade’s market positioning?
Alloy steel strip suits mid-to-high-end industrial blades and applications sensitive to customer downtime cost. General low-price blades can retain C75S as a product-line tier.
7. FAQ
Q: What is the difference between alloy steel strip for band saw blades and ordinary carbon steel strip?
A: The key difference is not simply “whether alloying elements are present,” but the fatigue–toughness–wear balance delivered by the alloy system. Plain carbon strip such as C75S meets general cutting needs; alloy grades such as 51CrV4 and 75Cr1 use Cr and V for hardenability and carbide effects, providing longer fatigue life and more stable edge retention in hardwoods and high-speed continuous cutting—reducing breakage and blade-change downtime.
Q: What is the typical hardness of steel strip for woodworking band saw blades?
A: Hardened and tempered alloy strip for woodworking band saw blades is commonly used at 43–48 HRC. Hardwood/high-load applications tend toward 45–47 HRC; thin-strip/high-toughness applications may use the lower end. Hardness must match tooth-setting and welding processes—higher is not always better.
Q: How do I choose between 51CrV4 and 75Cr1?
A: 51CrV4 offers better hardenability, tempering stability, and fatigue strength, making it suitable for thick strip, hardwoods, and high-speed sawmill lines where breakage risk is critical. 75Cr1 offers a better cost–performance balance for medium-to-high load woodworking blades and backing strip. If the dominant failure mode is tooth cracking or breakage, prioritize 51CrV4 and verify the supplier’s cleanliness control.
Q: How much can alloy steel strip improve blade life?
A: It depends on the cutting material, machine parameters, and baseline carbon grade. In hardwoods and abrasive composites, alloying combined with correct hardness and cleanliness control can typically extend useful cutting life to approximately 1.5–2× the carbon steel baseline, while reducing abnormal breakage-related failures. Specific values should be confirmed by customer-side comparative testing.
Q: What are the MOQ and lead time?
A: Standard MOQ is approximately 1 ton. For custom grades/sizes, lead time is typically 20–45 days depending on line scheduling. For demanding orders, specify at inquiry: grade, thickness × width, hardness window, edge condition, surface treatment, coil weight, and whether an EN 10204 3.1 MTC is required.


